Which material survives hydrochloric acid, sulphuric acid, chlorides, caustic and solvents? A practical corrosion guide to SS 316L, Duplex, Hastelloy, titanium, glass-lined and lined equipment for reactors, tanks, columns and heat exchangers in chemical plants.

For hydrochloric acid and strong chlorides, standard stainless steel (304, 316L) fails quickly; Hastelloy, titanium, glass-lined steel or rubber, PTFE or FRP lining are used instead. For sulphuric acid, the right material depends on concentration and temperature: carbon steel for concentrated cold acid, higher alloys or lined equipment for dilute or hot acid. Always confirm with corrosion data for your exact conditions.
In a chemical plant, the most expensive mistake is a vessel that corrodes through in a few months. A reactor, tank or heat exchanger does not fail because of pressure alone; it fails when the wall is thinned, pitted or cracked by the fluid it holds. Choosing the right material of construction (MOC) at the design stage protects safety, product purity and uptime. The correct choice depends on the chemical, concentration, temperature, velocity, presence of chlorides, impurities, oxygen and whether the service is continuous or intermittent. Because these factors interact, published corrosion tables are a starting point, not a final answer. Always confirm material choice with your process licensor, corrosion data or a corrosion specialist.
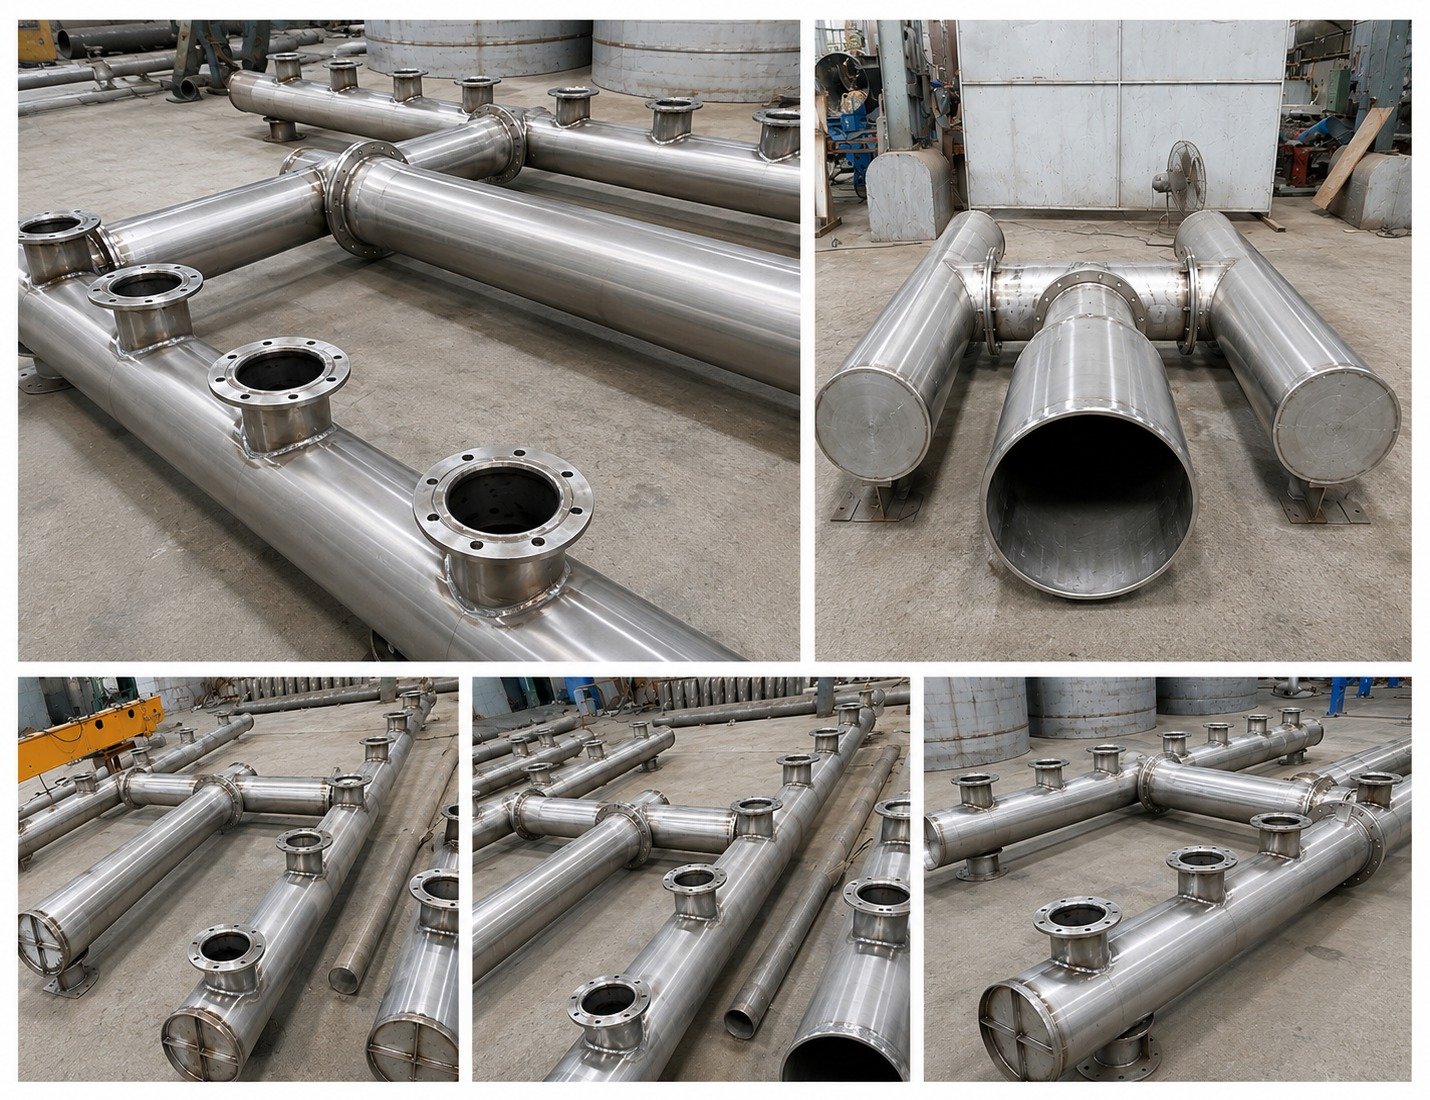
Creative Engineering fabricates equipment in SS 304, SS 316L, Duplex, Hastelloy, titanium, carbon steel and lined construction. Our material selection overview compares the main grades; this guide goes deeper into acids and chlorides.
| Type | What happens | Where it appears | Typical remedy |
|---|---|---|---|
| General corrosion | Even loss of wall thickness | Carbon steel in acids; stainless in strong acids | Corrosion allowance or a more resistant alloy |
| Pitting | Small deep holes | Stainless steel in chloride solutions | 316L, Duplex or Hastelloy; avoid stagnant liquid |
| Crevice corrosion | Attack under gaskets and deposits | Flanges, welds, under deposits | Better gasket design, cleanliness, higher alloy |
| Stress corrosion cracking | Cracking under tensile stress in a specific environment | 300-series stainless with chlorides at warm temperature | Duplex or nickel alloys, lower stress |
| Intergranular corrosion | Attack at grain boundaries after welding | Non-low-carbon stainless after welding | Use L grades (304L, 316L) or stabilised grades |
| Erosion corrosion | Wear from flow plus corrosion | Elbows, nozzles, agitators | Lower velocity, harder or better alloy |
| Galvanic corrosion | Two metals in contact in an electrolyte | Dissimilar metals joints | Insulate or match metals |

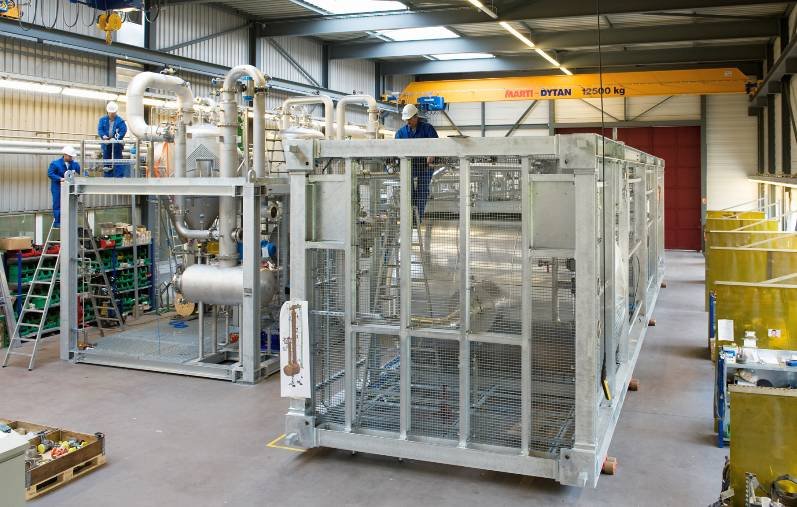
Hydrochloric acid is aggressive to nearly all stainless steels at almost any concentration, because chlorides break down the protective oxide layer. Even dilute, warm HCl can corrode 316L quickly. For this reason, HCl service usually uses non-metallic or highly alloyed materials:
Sulphuric acid behaves differently across its concentration range, so one material cannot be chosen without knowing both concentration and temperature. Strong, cold sulphuric acid (above about 90 percent) forms a protective film on carbon steel, so carbon steel tanks are widely used for storage. In the medium range, such as 40 to 80 percent, corrosion is more severe and carbon steel and many stainless steels are unsuitable; high-silicon iron, alloys such as Alloy 20 or Hastelloy, or lined construction are considered. Dilute sulphuric acid is aggressive to carbon steel but can be handled by certain stainless steels at lower temperature, or by lined and plastic equipment.
| Concentration | Typical option | Caution |
|---|---|---|
| Concentrated (above about 90%), cold | Carbon steel | Hot or diluted acid attacks quickly; avoid water ingress |
| Medium (about 40 to 80%) | Alloy 20, Hastelloy or lined steel | Aggressive; temperature has a large effect |
| Dilute (below about 30%) | 316L at low temperature, lined steel, FRP or PP | Check temperature and impurities |
| Oleum (fuming) | Carbon steel or special alloys | Specialist design needed |
Values above are general indications only. Final material selection must rest on corrosion data for your exact acid, temperature and impurities.
Chloride ions are a leading cause of pitting, crevice corrosion and stress corrosion cracking of stainless steel. Mild chloride exposure may be acceptable for SS 316L at low temperature, but higher chloride, higher temperature and low pH raise the risk sharply. In these cases, Duplex and super Duplex stainless steels, nickel alloys or titanium offer far better resistance. Titanium is widely used in seawater and brine heat exchangers because of its excellent resistance to chloride attack. For stressed parts such as welded vessels at elevated temperature, avoid 300-series stainless in chloride service unless the risk has been assessed. Clean equipment well after use and avoid leaving chloride-containing liquid to dry on surfaces.
When metals cannot economically resist the process, a lining or non-metallic material can be used. Glass-lined steel offers excellent resistance to most acids and is common in reactors for pharma and fine chemicals, but it is sensitive to thermal shock, impact and strong alkalis at high temperature. Rubber lining suits acid and chloride storage tanks at moderate temperatures. PTFE and PFA lining handles many aggressive chemicals but needs careful design to avoid permeation and vacuum collapse. FRP and polypropylene tanks are economical for atmospheric storage. Lined equipment needs strict handling, inspection and repair routines, and cannot be welded in the field once lined.
The cheapest material at purchase is often the most expensive over the life of the plant. A carbon steel vessel that corrodes in two years and needs replacement costs more than an alloy vessel that lasts fifteen. When comparing options, include purchase price, expected corrosion rate, inspection and maintenance cost, downtime, product contamination risk and replacement cost.
| Option | Relative cost | Typical strengths | Typical limits |
|---|---|---|---|
| Carbon steel | Low | Strong, economical, easy to fabricate | Corrodes in many acids and wet chlorides; may contaminate product |
| SS 304 / 304L | Medium | Good general resistance, hygienic | Weak against chlorides and strong acids |
| SS 316 / 316L | Medium to high | Better pitting resistance, pharma standard | Not for hot HCl or strong chlorides |
| Duplex and super Duplex | High | High strength, good chloride resistance | Needs controlled welding; temperature limits |
| Hastelloy and nickel alloys | Very high | Wide resistance, including many acids | High cost and long lead time |
| Titanium | Very high | Excellent in chlorides and oxidising media | Not for strong reducing acids |
| Glass or rubber lined steel | Medium to high | Resists many acids at lower cost than alloys | Handling and temperature limits, no field welding |
A short life-cycle cost comparison at the design stage often justifies a higher-grade material.
| Chemical | Common material options | Avoid or check |
|---|---|---|
| Dilute HCl | Glass-lined, rubber, PTFE, FRP, Hastelloy | SS 304 and 316L |
| Concentrated H2SO4 (cold) | Carbon steel | Water dilution, hot acid |
| Dilute H2SO4 | Lined steel, FRP, PP, Alloy 20 | Carbon steel |
| Nitric acid | SS 304L, 316L | Carbon steel |
| Acetic acid | SS 316L | Hot concentrated acid with contaminants |
| Chlorides, brine | Duplex, super Duplex, titanium | SS 304 |
| Caustic (hot, strong) | Nickel alloys | SS 304 and 316L at high temperature |
| Alcohols, ketones, esters | SS 304, 316L, carbon steel | Elastomer compatibility |
| Pharma solvents and APIs | SS 316L, electro-polished | Carbon steel contamination |
Treat this table as a guide only; every process has its own impurities and conditions.
See our GMP equipment design guide for surface finish and passivation details, and our inspection guide for corrosion monitoring in service.
Share your chemical list with concentrations, temperature range, pressure and cleaning methods, and our engineers will suggest suitable material options for your reactor, tank, column or heat exchanger. We can fabricate in stainless steel, Duplex, Hastelloy, titanium and carbon steel, and coordinate lined construction where required. Read our reactor price factors guide to see how material affects cost. Send your enquiry through the contact page or call +91 98251 38460. We are located in Ankleshwar, Gujarat, and serve plants across India.
Generally no. Hydrochloric acid and chloride-rich solutions corrode 316L quickly; lined equipment, Hastelloy or non-metallic materials are used instead.
It depends on concentration and temperature: carbon steel for cold concentrated acid, and alloys or lined and plastic equipment for dilute or hot acid.
Pitting forms small holes on an open surface, while crevice corrosion starts in shielded areas such as under gaskets and deposits.
Yes, titanium resists chloride attack very well, which is why it is used for seawater and brine exchangers, but it is not suitable for every acid.
It handles many acids in reactors for pharma and fine chemicals, but it is sensitive to impact and thermal shock.
Low-carbon grades such as 304L and 316L resist intergranular corrosion after welding.
Yes. We fabricate in SS 304, SS 316L, Duplex, Hastelloy, titanium and carbon steel, and can coordinate lined construction.
Creative Engineering, Ankleshwar, Gujarat designs and manufactures process equipment to ASME and IBR codes. Share your drawing or process data and our team will respond with a technical offer.

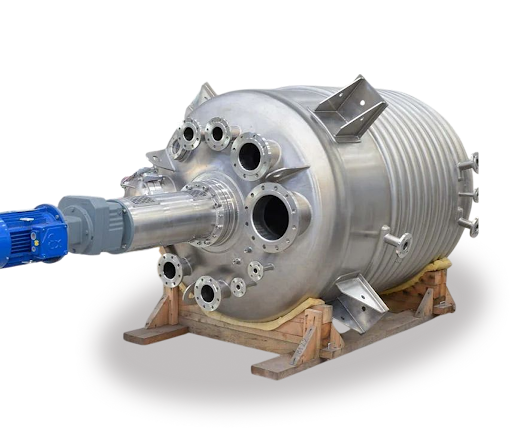 Reactor
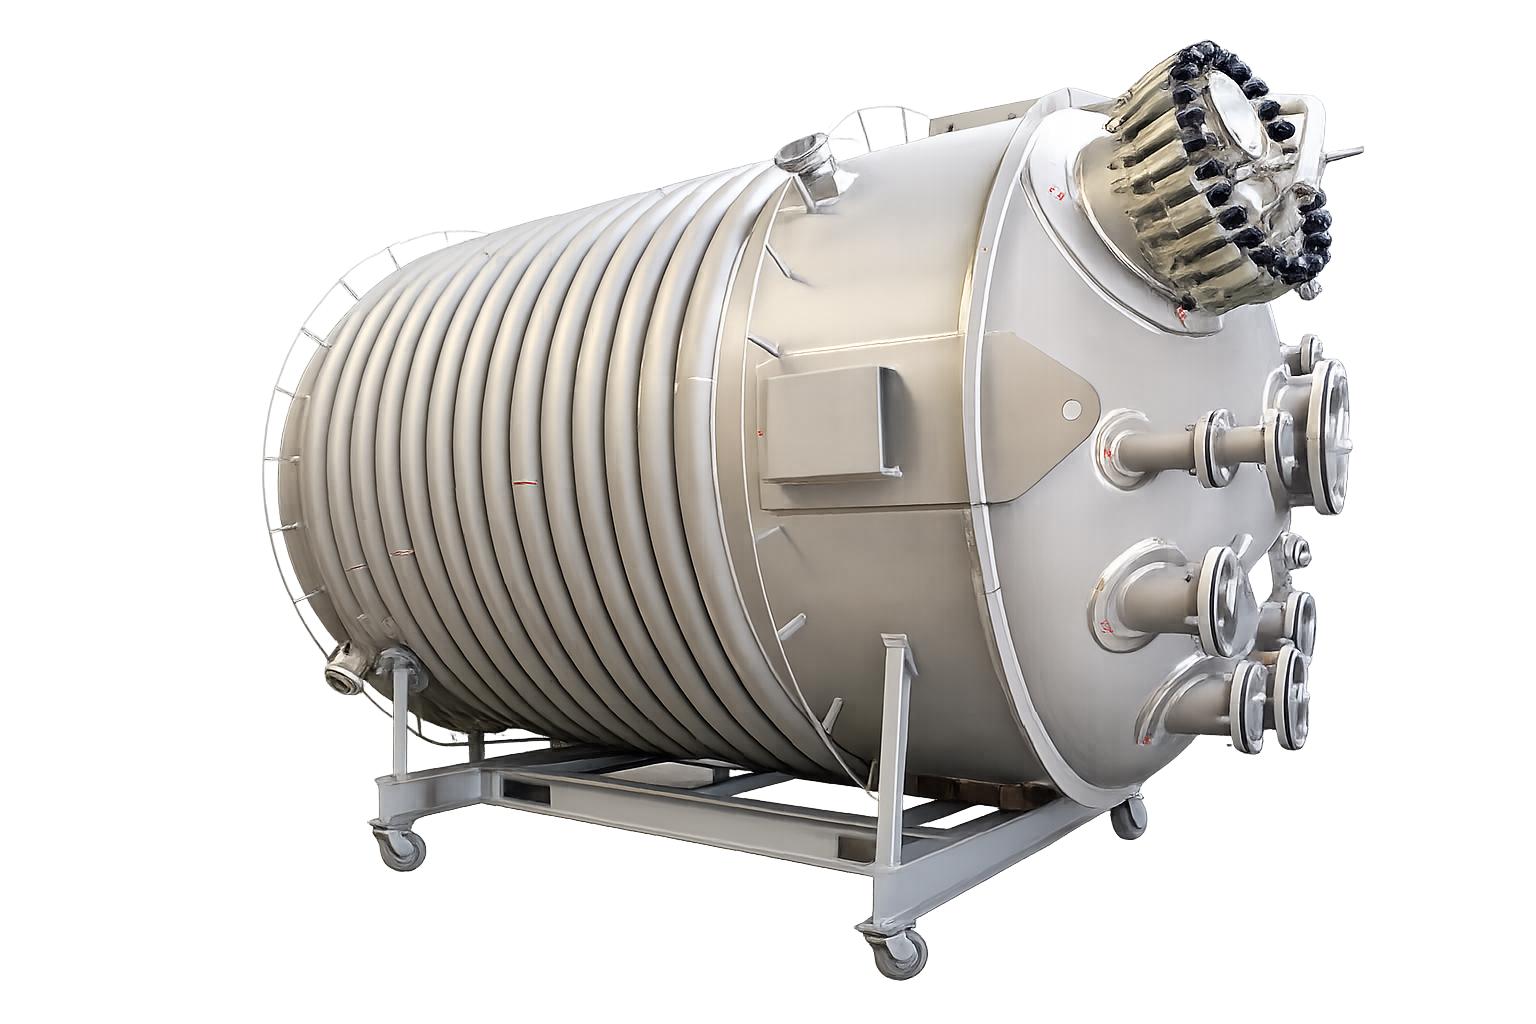 High Pressure Vessel
 Skid Equipment
 Receiver
 Heat Exchanger
 Pressure Vessel
 Silo
 Solvent Stripper
 Pharma Equipments