What a pipe spool is, how spools are fabricated and tested to ASME B31.3, which materials and welding methods are used, how isometric drawings work, what NDT and hydro testing involve, and how to choose a pipe spool fabricator in Ankleshwar, Gujarat and across India.

A pipe spool is a prefabricated section of piping made in a workshop from pipe, fittings and flanges, cut and welded to an isometric drawing, inspected and tested, then transported and joined on site. Fabricating spools in a controlled shop to ASME B31.3 improves weld quality, shortens site work and reduces cost compared with building all piping in the field.
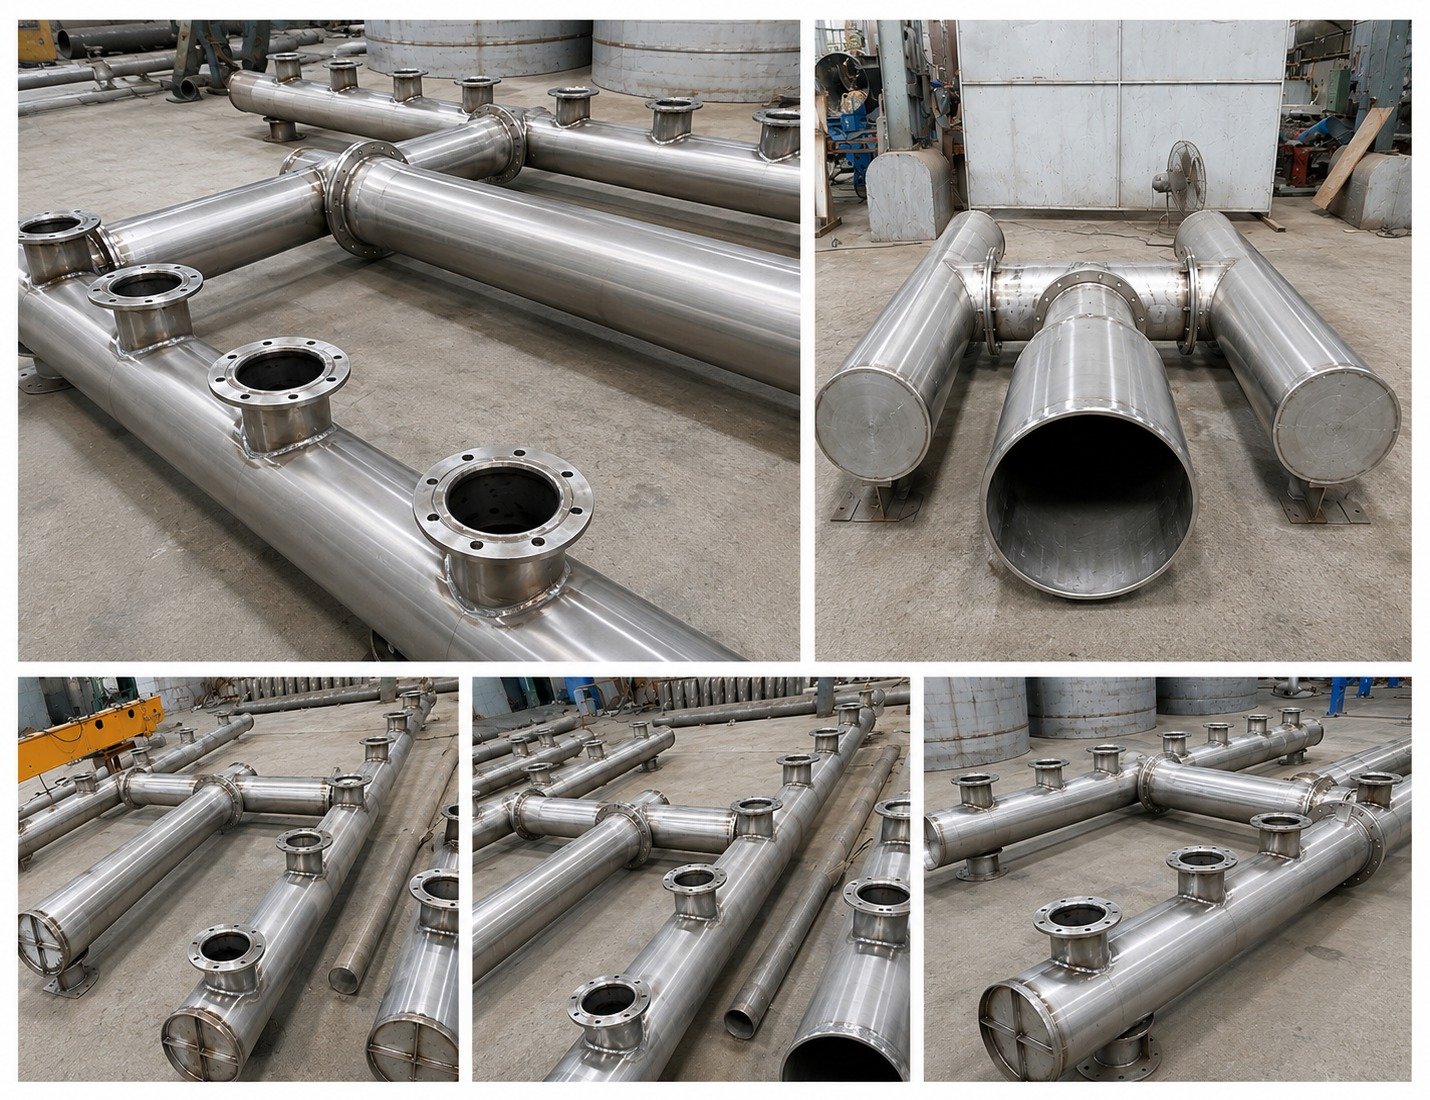
A pipe spool is a piece of piping that is fabricated away from the final installation location. It normally consists of straight pipe lengths, elbows, tees, reducers, flanges, branch connections and sometimes supports, all welded together according to a drawing. Once complete, the spool is cleaned, inspected, tested, marked and sent to the plant, where it is bolted or field-welded into the system. The word spool simply means a prefabricated piping assembly, and spool size is limited by what can be transported and lifted.
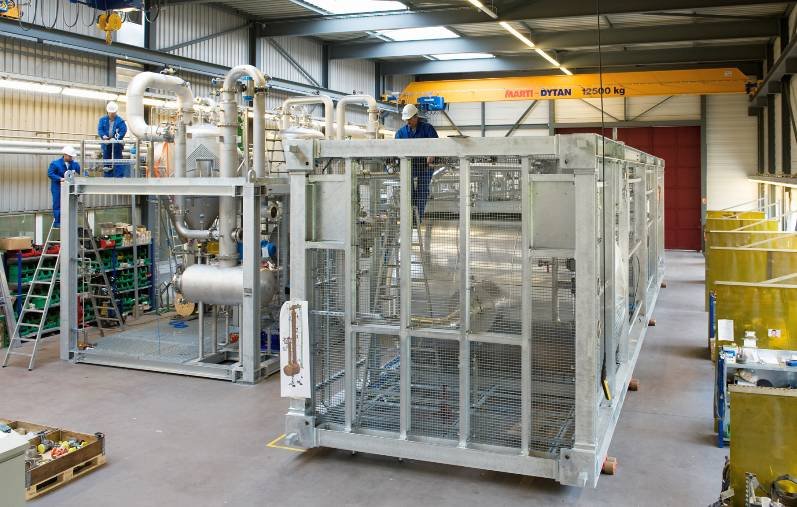
Chemical, pharmaceutical, petrochemical, oil and gas and utility plants use thousands of spools. Fabricating them in a workshop rather than in the field gives better access to the weld, cleaner conditions, controlled welding parameters and easier inspection. Creative Engineering fabricates spools at its units in Ankleshwar, Gujarat; see our pipe spool fabrication page.

ASME B31.3 is the piping code most used for chemical and pharmaceutical process plants, refineries and similar facilities. It covers design, materials, fabrication, assembly, erection, examination, inspection and testing of piping. The code classifies fluids into categories, from Normal Fluid Service to Category D, Category M and High Pressure services, with stricter requirements for more hazardous fluids. Wall thickness is calculated from design pressure, temperature, material allowable stress, corrosion allowance and joint quality factor. Always follow the edition of the code and the design basis stated by your engineer.
| Topic | What B31.3 addresses | Why it matters for spools |
|---|---|---|
| Design | Pressure, temperature, thickness, flexibility and supports | Defines the wall thickness and fittings to be used |
| Materials | Permitted grades and allowable stress | Controls which pipe and fittings can be bought |
| Fabrication | Welding, bending, forming and joining | Sets the welding procedure and welder qualification rules |
| Examination | Visual, radiography and other NDT extents by fluid service | Decides how many welds are tested |
| Testing | Hydrostatic or pneumatic leak and strength test | Defines test pressure and hold time |
Every spool is built from a limited set of components. Knowing them helps you read a quotation and compare offers.
| Component | Standard (typical) | Purpose |
|---|---|---|
| Pipe | ASTM A106, A53, A312 | Carries the fluid; size by nominal bore and schedule |
| Elbows (45, 90 degree) | ASME B16.9 | Changes direction |
| Tees and reducers | ASME B16.9 | Branches and size changes |
| Flanges (weld neck, slip-on, blind) | ASME B16.5 | Bolted joints to equipment and valves |
| Branch connections | Weldolet, sockolet, stub-in | Instrument and drain connections |
| Gaskets and bolting | ASME B16.20, B16.21 | Seal flanged joints |
| Pipe supports and shoes | Per piping drawing | Carry weight and limit movement |
Flange rating (Class 150, 300 and above), face type (raised face, flat face, ring-type joint) and bolt material must match the equipment nozzle connection.
Spools are made from isometric drawings (isos), which show the piping in a 3D-style single-line view with dimensions, line numbers, flow direction, pipe size, schedule, material, fittings, flanges, weld locations and a bill of materials. A good iso identifies each spool number, field welds, shop welds, orientation of flanges and branches, slope, supports and insulation or painting requirements. Before cutting any pipe, the fabricator checks the iso against the piping and instrument diagram (P and ID), the line list and the material specification.
The correct material depends on the fluid, temperature, pressure and corrosion allowance. Common choices include carbon steel pipe (for example ASTM A106 Grade B or A53), stainless steel pipe (ASTM A312 TP304, 304L, 316 or 316L), low-temperature carbon steel, alloy steel and Duplex stainless steel. Fittings follow standards such as ASME B16.9, flanges follow ASME B16.5 and gaskets and bolts are selected to match. For corrosive chemicals, lined pipe, Hastelloy or titanium may be used. Read our material selection guide for more.
| Material | Typical use | Note |
|---|---|---|
| Carbon steel (A106 Gr B, A53) | Steam, water, non-corrosive hydrocarbons | Economical, needs coating or paint |
| SS 304 and 304L | General chemical and food service | Not suited for strong chlorides |
| SS 316 and 316L | Pharma, acids, chloride-bearing fluids | Default for GMP and API plants |
| Duplex | High-strength, chloride service | Needs controlled welding procedure |
| Alloy steel | High-temperature service | May need heat treatment |
| Hastelloy, titanium | Aggressive acids, special duties | Higher cost; specific welding skills |
Pipe welds are normally made with TIG (GTAW) for the root pass and either TIG or MIG/MAG or stick (SMAW) for fill and cap passes, depending on material and thickness. Stainless steel spools often use TIG with argon back-purging so the inside of the weld is bright and free of oxide. Each weld must follow a welding procedure specification (WPS) backed by a procedure qualification record (PQR), and welders must be qualified for the process, position and material. Welds are identified with welder IDs and recorded on a weld map linked to the spool number. Our welding system follows ISO 3834 practice; see our certifications.
B31.3 requires examination appropriate to the fluid service. Typical checks include visual examination of all welds, radiographic (RT) or ultrasonic (UT) testing of a percentage of butt welds, and dye penetrant (PT) or magnetic particle (MT) on selected welds. Spools are then pressure tested, normally with water (hydrostatic) at the code test pressure and held for a set time while joints are inspected for leaks. For lines that cannot be filled with water, a pneumatic test with extra precautions or an alternative leak test may be used. See also our inspection and hydro testing guide.
A fabricator with a documented quality plan catches most of these in the shop, long before the spool reaches the plant. See our quality policy.
Creative Engineering can supply spools along with vessels, heat exchangers and skid-mounted process equipment, so the whole package arrives from one source. Send your isometrics and line list on the contact page or call +91 98251 38460.
Pipe spools are often supplied with skid packages, where piping, valves and instruments are pre-assembled on a steel frame, and as part of complete plant piping for reactors, distillation columns and utility systems. For export orders the spools are packed to suit sea transport, with documentation to the standard asked by the buyer. Read our export guide and our Gujarat manufacturers guide for details.
It is the prefabrication of piping sections in a workshop to an isometric drawing, followed by inspection, testing and dispatch to site.
ASME B31.3 is the most widely used code for chemical and pharmaceutical process piping.
Carbon steel, stainless steel 304 and 316L, alloy steel, Duplex and special alloys such as Hastelloy, chosen to suit the fluid and temperature.
Visual examination, radiography or ultrasonic testing of a percentage of welds, dye penetrant testing where needed, and a hydrostatic pressure test.
An isometric drawing with dimensions, material, fittings, weld locations and a bill of materials.
Yes. We fabricate carbon steel and stainless steel pipe spools in Ankleshwar, Gujarat for plants across India and for export.
Isometric drawings or a line list with pipe size, schedule, material, flange rating, test and NDT requirements, painting and delivery date.
Creative Engineering, Ankleshwar, Gujarat designs and manufactures process equipment to ASME and IBR codes. Share your drawing or process data and our team will respond with a technical offer.

 Reactor
 High Pressure Vessel
 Skid Equipment
 Receiver
 Heat Exchanger
 Pressure Vessel
 Silo
 Solvent Stripper
 Pharma Equipments