What makes process equipment GMP-compliant: material, surface roughness (Ra), electro-polishing, crevice-free welds, drainability, dead legs, CIP and SIP, passivation, qualification documents and how to specify GMP reactors, Nutsche filters, tanks and skids.
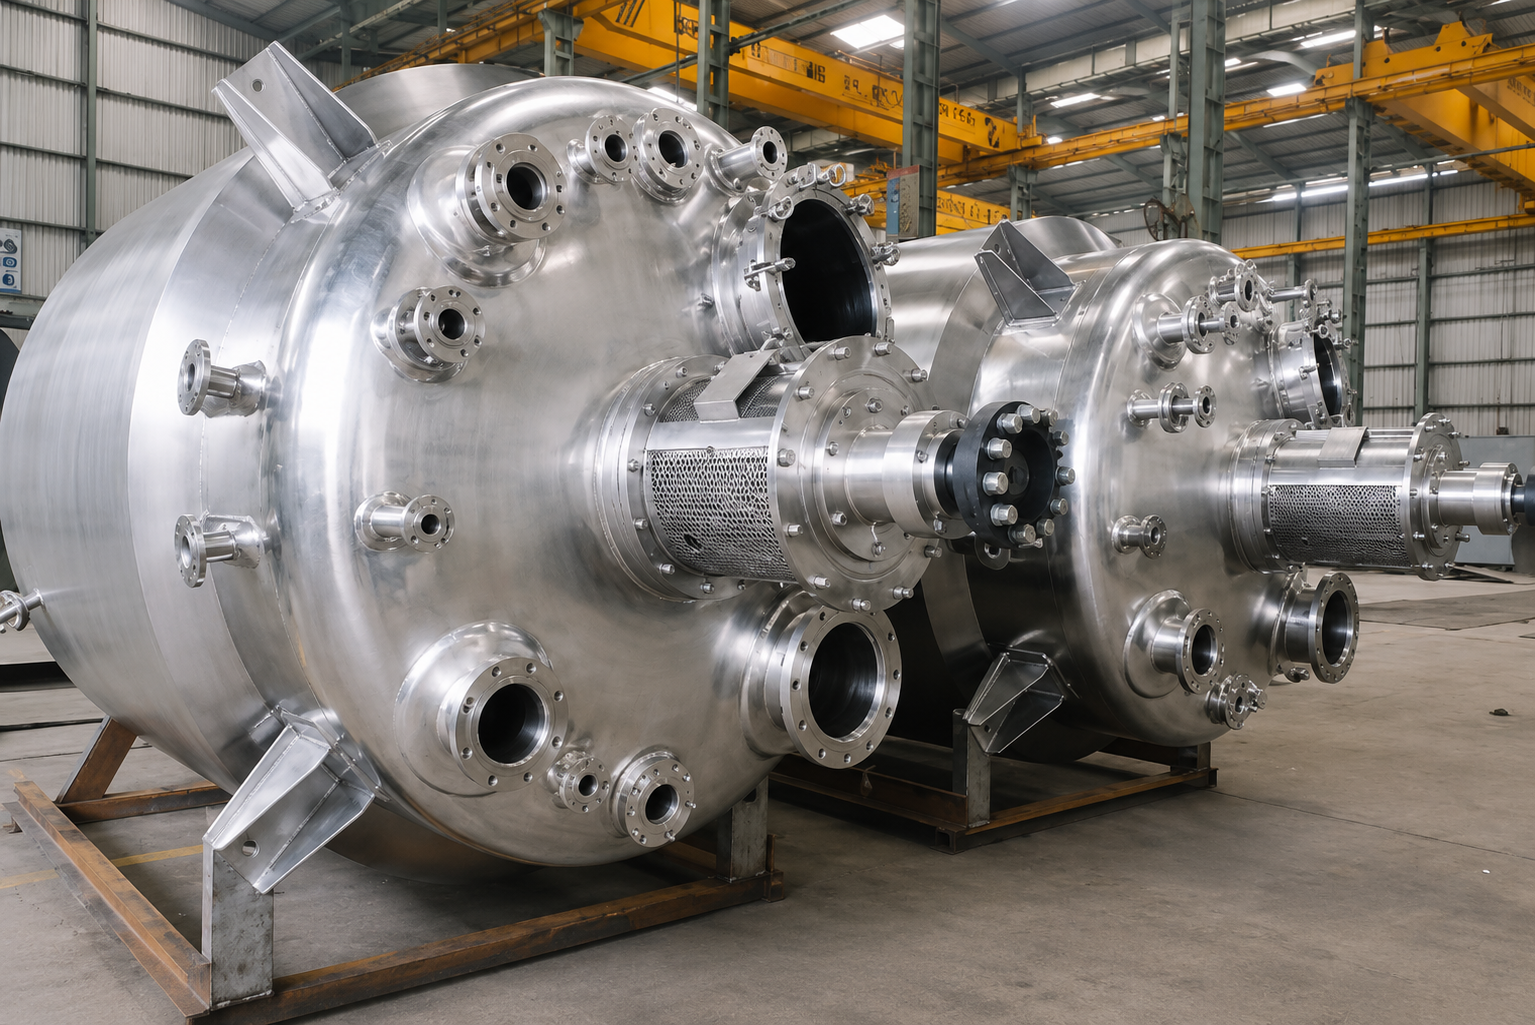
GMP-compliant process equipment is made from corrosion-resistant material (usually SS 316L), has smooth, cleanable product-contact surfaces (often electro-polished to Ra 0.4 micron or better), crevice-free welds, self-draining geometry, no dead legs, supports for CIP and SIP, and a documentation package (material certificates, finish reports, drawings) that supports IQ, OQ and PQ.
GMP stands for Good Manufacturing Practice, a set of principles and regulations that ensure pharmaceutical products are made consistently to quality standards. GMP does not publish a single list of equipment specifications, but its principles are clear: equipment must not contaminate the product, must be cleanable to a validated level, must be made of suitable material, and must be documented and maintained. In practice, buyers translate these principles into design requirements: smooth surfaces, no hiding places for product, materials that do not react with the product or the cleaning agents, and complete traceable records.
Pharmaceutical manufacturers in India typically follow national schedules and international expectations such as those of WHO, the US FDA and European authorities, and for bioprocess and some pharma equipment the ASME BPE (Bioprocessing Equipment) standard is a common reference. Always follow the requirements of your own quality department and regulators; the guidance below shows how manufacturers like Creative Engineering support those requirements in fabrication.
| Pillar | Requirement | How it is delivered |
|---|---|---|
| Material | Non-reactive, corrosion-resistant, traceable | SS 316L (or higher alloy) with mill test certificates |
| Surface | Smooth, non-porous, easy to clean | Mechanical polish and electro-polishing to a defined Ra |
| Geometry | No crevices, no dead legs, self-draining | Radiused corners, sloped bottoms, flush welds, correct nozzle design |
| Cleanability | Cleaned and sanitised without disassembly | CIP spray devices, SIP-capable design, drain valves at low points |
| Documentation | Proof that it was built as specified | Material certificates, finish reports, weld records, drawings, qualification support |
SS 316L resists pitting and crevice corrosion better than 304 because it contains molybdenum, and its low carbon content avoids carbide precipitation at welds. Product-contact parts in most pharma reactors, filters and tanks are therefore SS 316L. For very aggressive chemistry, such as chlorinated solvents or strong acids in API synthesis, higher alloys like Hastelloy or Duplex, or lined construction, may be selected. Non-product-contact parts such as jackets and frames may be SS 304 or carbon steel to save cost. Read our material selection guide for details.
Ra is the average roughness of a surface, measured in micrometres (µm) or microinches. A lower Ra means a smoother surface that offers fewer places for product and microorganisms to cling. Typical stainless steel finishes are:
| Finish | Typical Ra | Use |
|---|---|---|
| Mill finish or blasted | High, not specified for hygiene | Non-hygienic, utility, outer surfaces |
| Mechanical polish | About 0.8 µm or better (grit-dependent) | General pharma and food product contact |
| Mirror polish | About 0.4 µm or better | High-purity, easy-clean surfaces |
| Electro-polish (EP) after mechanical polish | About 0.4 µm or better, microscopically smoother | GMP and sterile service |
Electro-polishing is an electrochemical process in which the stainless steel part is made the anode in an acid bath and a small layer of surface metal dissolves. Microscopic peaks dissolve faster than valleys, so the surface becomes smoother and brighter. It also removes embedded iron and surface contaminants and leaves a chromium-rich passive layer. The benefits are a lower effective roughness, reduced product adhesion, easier cleaning and improved corrosion resistance. Electro-polishing is applied after mechanical grinding and buffing and does not hide poor welds, so weld quality must be right first. Creative Engineering performs buffing and electro-polishing in-house, with pickling and passivation available.
Welding and grinding disturb the thin chromium oxide layer that protects stainless steel. Pickling removes weld heat tint and scale using an acid paste or bath, and passivation then helps the chromium-rich passive film re-form evenly so the surface resists rust and staining. For GMP service, these steps are normally carried out after fabrication and before electro-polishing or final cleaning, and records are kept so that the buyer can show the treatment was done. Skipping pickling and passivation is a common reason for rouging and spotting in otherwise well-built equipment.
A dead leg is a section of piping or a branch where fluid can stagnate because it is not part of the main flow. Product and cleaning agent can remain trapped in a dead leg, giving a route for contamination or microbial growth. Good GMP design keeps branches as short as possible, with a recognised rule of thumb that the length of a branch beyond the main pipe should be limited relative to its diameter (shorter ratios are preferred and some standards ask for very low ratios). Zero dead-leg piping uses special fittings and valves that sit flush with the main line. In process skids, we route piping to avoid pockets and provide drains at every low point.
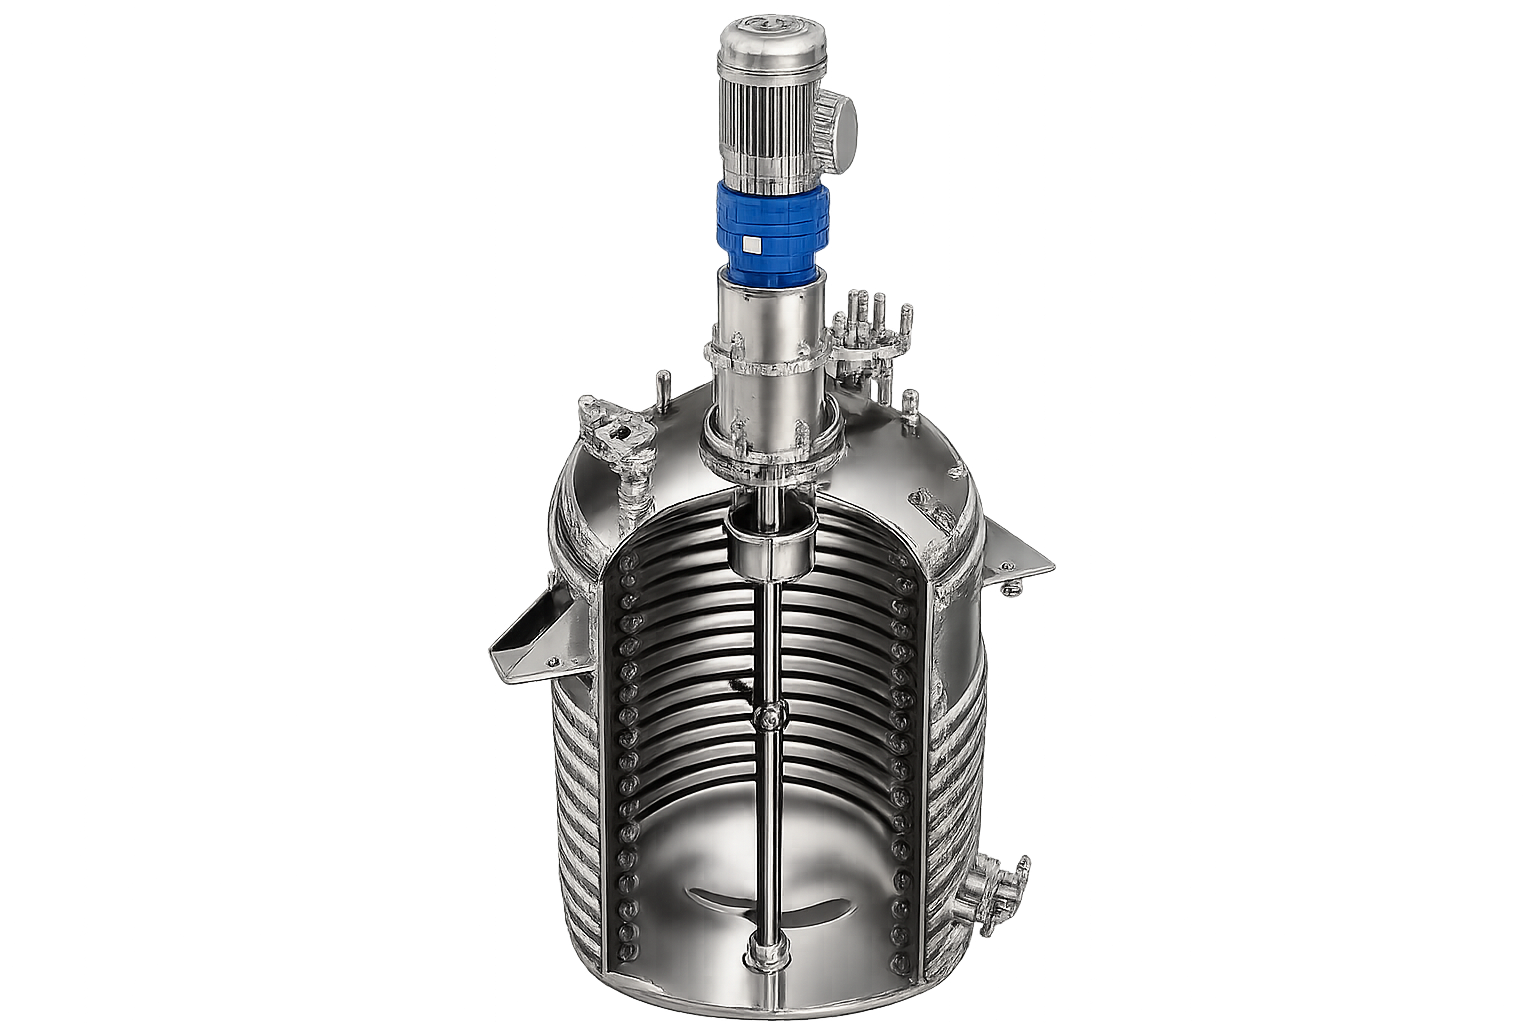
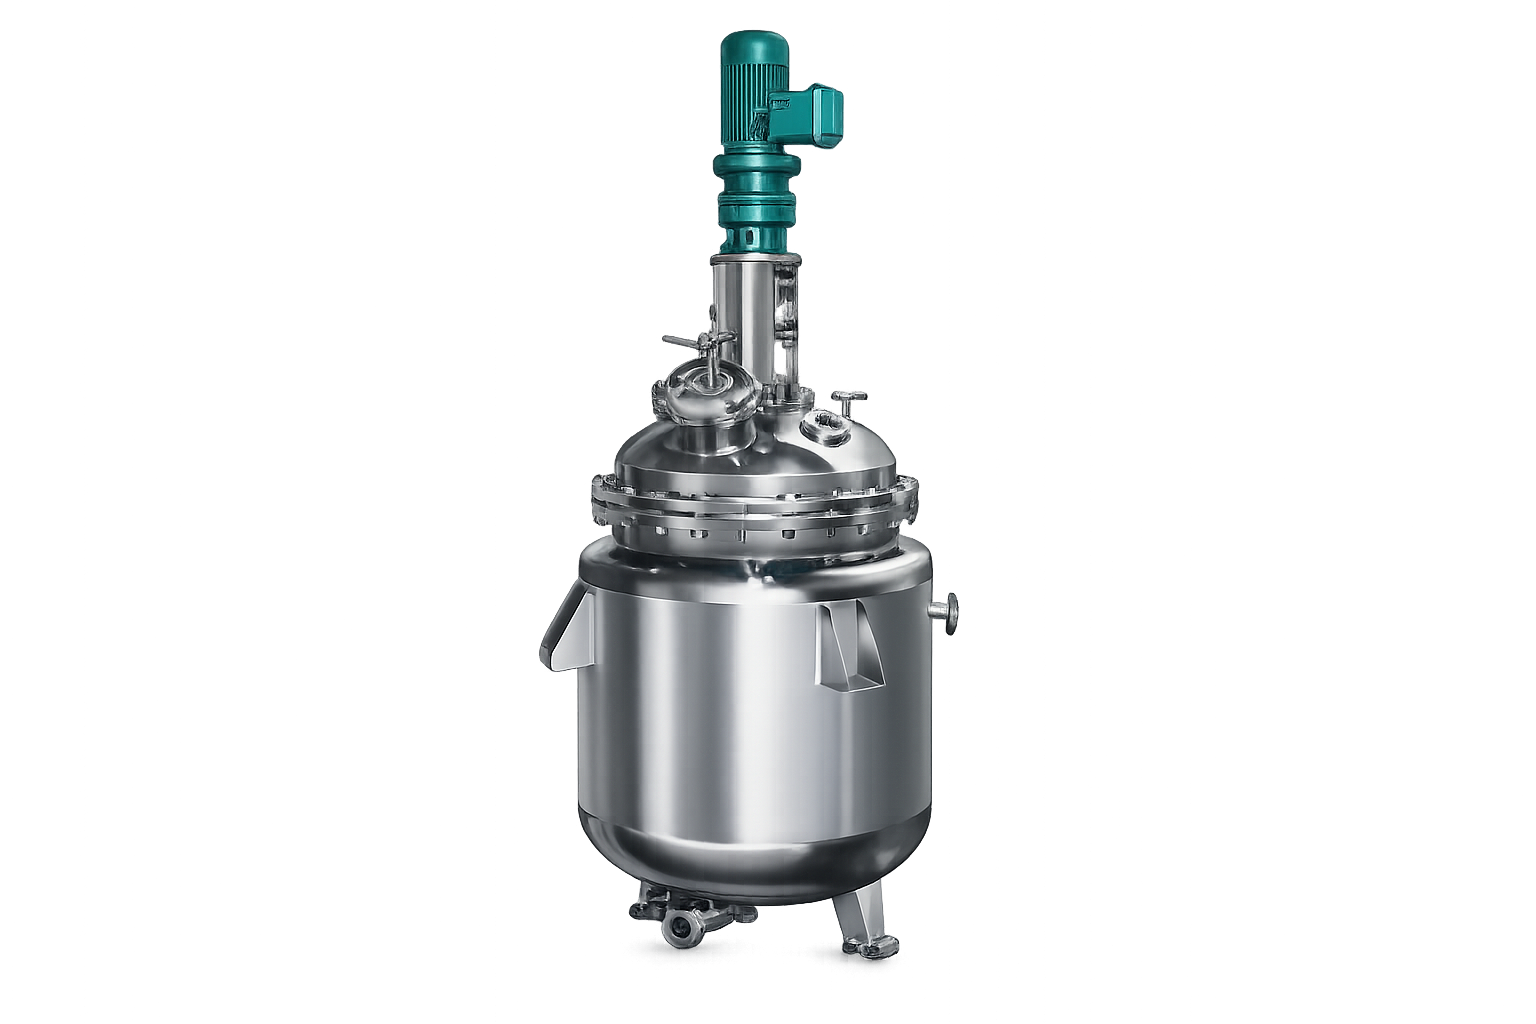
A reactor is only as hygienic as its weakest component. Agitator shafts, mechanical seals, sight glasses, manways and instrument connections all touch the product or its vapour. Choose mechanical seals with suitable face and elastomer materials, and keep seal-support systems clean and well documented. Select gaskets and O-rings that are compatible with the product and the cleaning chemicals, and keep a record of their material. Use hygienic instrument connections, flush-mounted where required, so that probes do not create pockets. Read how agitation affects mixing in our reactor guide.
CIP (clean-in-place) washes equipment with water and cleaning solutions without dismantling it. A reactor or tank prepared for CIP has spray balls or nozzles that wet all internal surfaces, a drain at the lowest point, and surfaces and welds that can be cleaned effectively. SIP (sterilise-in-place) uses clean steam to sterilise equipment in position. Equipment for SIP must withstand the temperature and pressure of the steam, have condensate drain points, and be designed so air can be vented and no cold spots remain. Both procedures must be validated by the user; the manufacturer's job is to supply equipment that makes validation straightforward.
A complete dossier shortens the time between delivery and production start. See how documentation is handled under our quality policy. For skids, read what is skid-mounted process equipment.
Visit our pharma equipment page and API intermediates page or send your URS through the contact page.
A clear User Requirement Specification (URS) saves weeks of back-and-forth. It tells the fabricator what you need and how you will check it. Include the following so that the quotation and drawing match your expectation the first time:
Send these details through the contact page or call us on +91 98251 38460 and our engineers will respond within 24 hours.
Our team reviews these points at the drawing stage so that problems are fixed before steel is cut. See our customised equipment options for non-standard designs.
It means the equipment is built from suitable material, has cleanable and non-contaminating surfaces, is documented and traceable, and supports validation, so that it does not compromise product quality.
SS 316L resists pitting and crevice corrosion better than 304 and welds without carbide precipitation, making it the default for product-contact surfaces.
An electrochemical process that smooths stainless steel by dissolving surface peaks, improving cleanability and corrosion resistance.
Ra is the arithmetic average roughness of a surface. Lower Ra means smoother surfaces that are easier to clean.
A dead leg is a branch or pocket where fluid can stagnate because it is not in the main flow, creating contamination risk.
CIP is cleaning in place with water and chemicals, while SIP is sterilising in place with clean steam or other methods.
Material certificates, drawings, weld and NDT records, finish and passivation reports, calibration certificates and test records support qualification.
Yes. Electro-polishing and buffing are carried out in-house, and pickling and passivation are available for stainless steel equipment.
Lead time depends on size, material and finish. Share your URS and our team will confirm the schedule in the quotation.
Creative Engineering, Ankleshwar, Gujarat designs and manufactures process equipment to ASME and IBR codes. Share your drawing or process data and our team will respond with a technical offer.

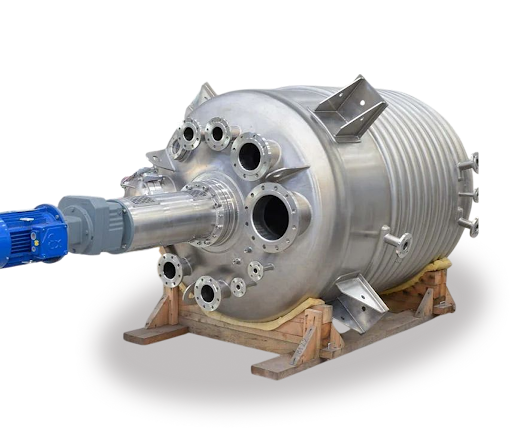 Reactor
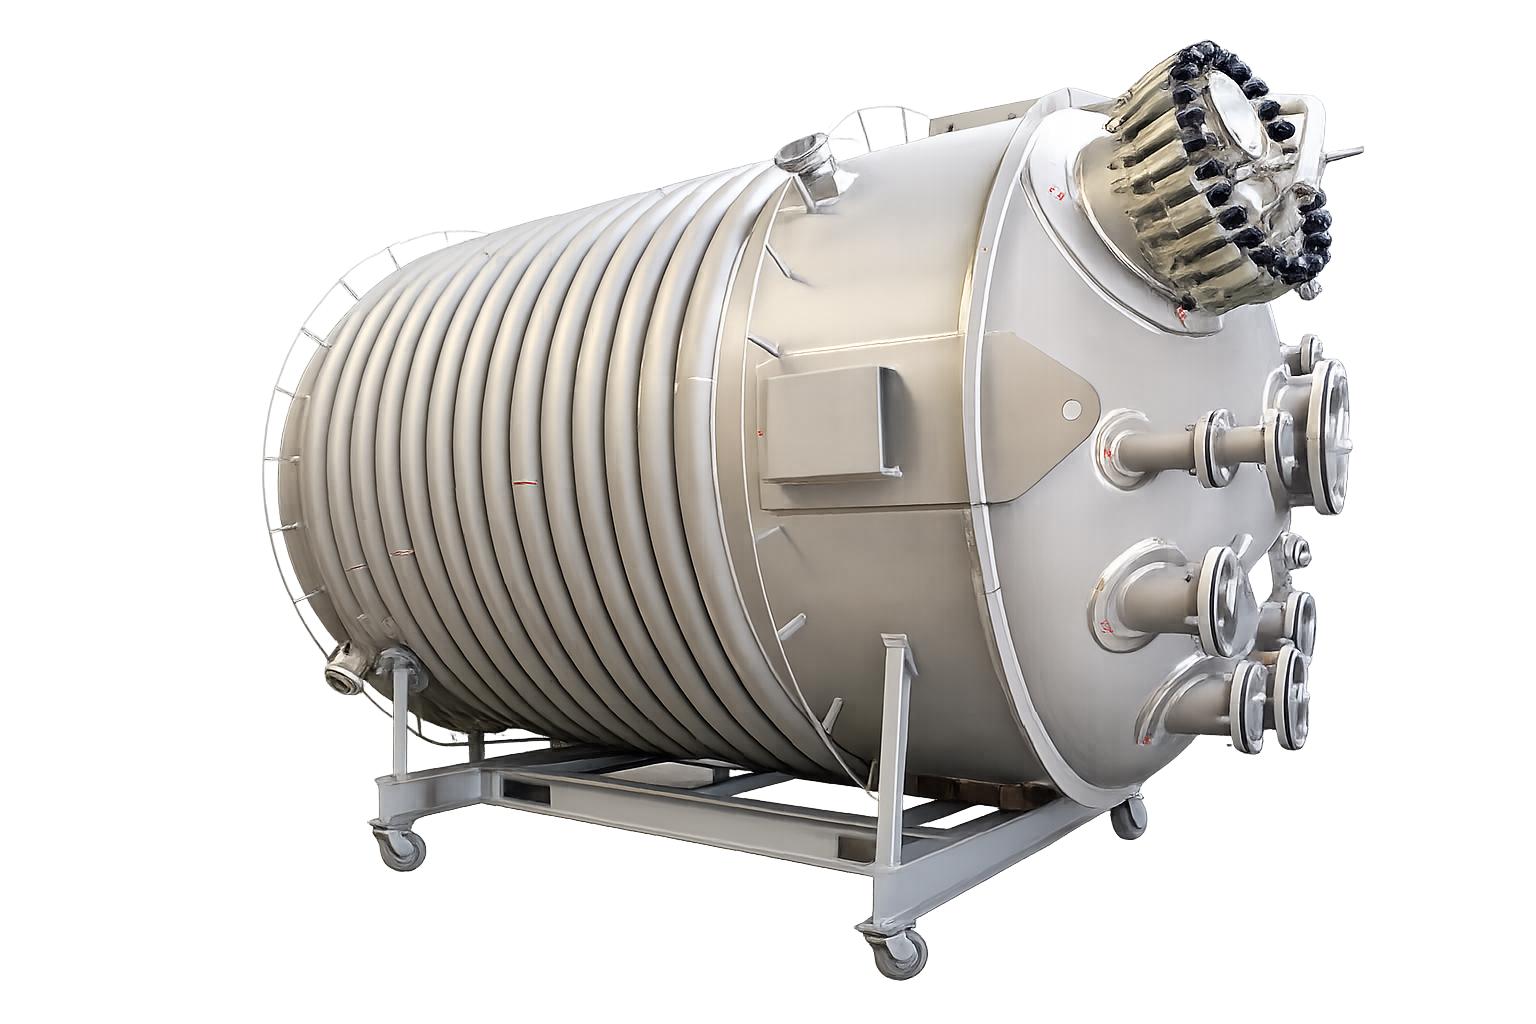 High Pressure Vessel
 Skid Equipment
 Receiver
 Heat Exchanger
 Pressure Vessel
 Silo
 Solvent Stripper
 Pharma Equipments